timesupmag
  • Home
  • Business
  • Featured
  • Global Trade
  • Industry
  • Life
  • Market
  • Tech
  • Travel
Author

Sandra

Sandra

Global Trade

400W-Class Servo Wheels for Compact Automation: Solving AGV Drive Challenges

by Sandra October 11, 2026

Problem: Compact AGVs need full drive capability in tight envelopes

Small automated guided vehicles face three immediate constraints: limited space, limited cooling, and the need for precise motion control under variable loads. Designers who try to shoehorn a separate motor-plus-gearbox assembly often hit mechanical layout and thermal ceilings. An integrated agv drive wheel that packages torque, encoder feedback, and mounting into a single unit addresses those constraints directly; the same product positioning is reflected where a dedicated servo wheel for AGV is required for repeatable path following. I observed the same trade-offs during a pilot demonstration at Hannover Messe, where compact logistics platforms highlighted the difference between bulky drivetrains and integrated wheel solutions.

agv drive wheel

Technical checklist for specifying a 400W-class servo wheel

Specify these items before selecting components:- Continuous torque and peak torque ratings tied to worst-case acceleration and incline requirements; size components to handle peak loads without thermal derating.- Encoder resolution and communication interface (incremental vs. absolute; TTL/SSI/CANopen); match these to your motion controller for closed-loop stability.- Thermal path and IP rating; pad designs and mounting faces must transfer heat to the chassis when airflow is limited.- Brake requirements and regen behavior; decide whether mechanical brakes or controlled electronic holding are necessary.- Bearing life and radial load capacity; lateral forces from steering or minor impacts shorten wheel bearings quickly if underrated.Each bullet above is measurable. Use test cycles that reflect your duty profile rather than relying on nominal specs.

Common pitfalls and practical fixes

Pitfall: Overestimating onboard cooling. Fix: Add thermal interface to chassis and limit continuous torque through control logic.Pitfall: Choosing too-fine encoder resolution without matching controller bandwidth. Fix: Balance encoder counts with controller update rate to prevent noise amplification.Pitfall: Neglecting lateral loads from turning or uneven floors. Fix: Increase bearing spec and include a compliance element between wheel and frame.Pitfall: Assuming identical torque across speeds. Fix: Validate torque-speed curve under expected voltage and temperature ranges.These are operational, testable items. Implement each fix during prototype runs to avoid late-stage rework.

Comparative insight: integrated servo wheel versus alternatives

Integrated servo wheel- Pros: compact footprint, fewer mechanical interfaces, simpler alignment, often built-in encoders and brakes.- Cons: limited modularity for repair, higher initial unit cost.Separate motor + gearbox- Pros: easy part swapping, flexible motor selection.- Cons: alignment complexity, larger envelope, added backlash.Hub motors and in-wheel drives- Pros: minimal external gearing, very compact.- Cons: cooling limits and sometimes lower peak torque.Match choice to program priorities: space and reliability favor integrated servo wheels; maintainability and upgrade flexibility favor modular assemblies.

Testing and deployment checklist

Run these tests before large-scale rollout:- Thermal soak under maximum continuous torque for the expected duty cycle.- Encoder and control loop stability tests with simulated load disturbances.- Mechanical shock and bearing fatigue tests reflecting your facility floor.- Emergency-stop torque retention and brake release timing validation.Document results and set pass/fail thresholds tied to mission-critical metrics, not vendor datasheet claims.

Conclusion and pragmatic recommendation

When compact AGVs must deliver accurate motion, predictable thermal behavior, and a small mechanical footprint, choosing a 400W-class integrated servo wheel reduces design risk if you follow a clear specification and testing sequence. That sequence — torque and thermal sizing, encoder-match validation, bearing and lateral-load checks, and duty-cycle testing — solves the core problems that derail many projects. For teams that need component-level support and proven integration options, Kinco offers a coherent set of wheel-motor assemblies and documentation that align with these pragmatic requirements.

October 11, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

A Practical Guide to Procuring 20 Hydraulic Modules for Your Production Line

by Sandra August 26, 2026

Start with what your line actually needs

When you plan to source 20 new modules, the starting point is the shop floor — the rhythms, takt, and the weak links. Begin by mapping cycle times and duty cycles for the processes that will use a hydraulic machine system. That grounding keeps decisions practical: pump displacement and cylinder stroke matter because they determine throughput and thermal load. I’ve seen teams overspecify capacity to “cover future loads” and end up with wasted cost and control headaches; the reverse — underspecifying — creates downtime and scrap.

hydraulic machine system

User-centric checklist for sourcing 20 units

Think of this as a short, ordered plan you can give to purchasing and engineering together. Capture: operational hours, maximum pressure, typical hydraulic fluid viscosity range, mounting constraints, and spare-parts access. Add test acceptance criteria (run-in hours, leak rate, control valve response) and a delivery schedule tied to line ramp points. On the paperwork side, require a clear parts list and service manual so maintenance can trace actuator, pressure relief valve, and manifold layouts without calling the vendor every week.

How to vet suppliers calmly and efficiently

Assess supplier fit through three lenses: product fit, proven production history, and spare-part logistics. Visit or request video of the supplier’s assembly area — real-world anchors matter; for many teams after the Port of Shanghai congestion in 2020, seeing storage practices and packing lists reassured them that shipments would arrive intact. Ask for references from shops that run similar cycle rates and ask about mean time between failures. Request sample validation: one assembled module, instrumented for a brief factory acceptance test so you can measure control valve hysteresis and pump vibration before committing to 20.

Common mistakes teams make — and how to avoid them

People often bundle too many specs into a single contract and then micromanage vendors on minor details, which leads to late deliveries. Another repeated error is ignoring lifecycle spares — order essential items like seals and filters with the first shipment. Take the time to define acceptance tests with explicit pass/fail thresholds for leak rate and control response. — Also, be explicit about lubrication and filtration requirements so hydraulic fluid contamination doesn’t become a chronic failure mode.

Alternatives and small-scale experiments

If buying 20 at once feels risky, stagger deliveries: 4, then 8, then 8. Use the initial batch to validate installation ergonomics and mounting brackets. Consider mixed sourcing: a primary vendor for 12 modules and a reliable secondary for 8 to hedge lead-time risk. Compare integrated manifold solutions against modular valve stacks on metrics like footprint, serviceability, and cost-per-cycle. Keep an eye on actuator responsiveness during pilot runs; sometimes a slightly higher pump displacement smooths control without large energy penalties.

Operational teardown notes

When you disassemble a pilot unit, document torque specs, seal part numbers, and routing for hoses and return lines. In the operational production teardown, note {main_keyword} and {variation_keyword} and record them alongside measurements such as pressure setpoint drift over 1,000 cycles. This creates a concise baseline for warranty claims and continuous improvement efforts.

hydraulic machine system

Advisory: three golden rules for final selection

1) Match duty to design: select modules whose rated continuous pressure and cylinder stroke exceed your measured peak demands by a modest margin — not by an order of magnitude. 2) Prioritize maintainability: require modular manifolds, clearly labeled ports, and accessible pressure relief valves so a technician can swap a component within a shift. 3) Secure logistics: confirm spare-part lead times and local stocking plans; aim for critical spares within 72 hours locally and secondary spares within 14 days internationally.

Closing thought

Source deliberately, validate early, and protect uptime with parts and procedures that your team trusts — that’s how 20 modules become a steady asset rather than a recurring headache. Intake. —

August 26, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

Balancing Bite and Bread: How Cost and Performance Shape a Commercial Classroom 3D Printer

by Sandra August 7, 2026

The classroom hum should feel like a kitchen at midday — warm, focused, a little fragrant with melting filament — and the best 3D printers achieve that without breaking the budget. This comparative look slices through build volume, layer height, and ongoing consumables to show where money buys real classroom value. Early on, consider the role of reliable slicing tools; a friendly slicer and tidy workflow matter as much as the machine itself, so try pairing hardware with proven 3d printer software to keep teachers and students moving through projects with confidence.

What to Compare First: Hardware vs. Ongoing Costs

Touch the printer frame — is it steel, or thin sheet metal? That tactile difference hints at durability. Compare these categories side-by-side: initial purchase (chassis, stepper motors, hotend), consumables (filament type and spool life), and maintenance (nozzle swaps, bed replacement). Build volume governs what students can actually make; a generous build volume costs more but reduces the need to split prints. Watch filament types — PLA feels forgiving and smells faintly sweet when heated; ABS offers strength but needs enclosure and ventilation. Factor in slicer compatibility and how the machine handles G-code from classroom projects. In an operational production teardown, {main_keyword} and {variation_keyword} often emerge in cost models as hidden line-items: consumable life and teacher time spent on troubleshooting.

Performance Levers That Matter

Performance isn’t a single figure. It’s a blend: print speed, accuracy at thin layer heights, bed adhesion, and repeatability across dozens of prints. A nozzle that clogs mid-class is a moment lost — the hum stops, students drift. Choose extruders and nozzles designed for classroom throughput. FDM machines that sustain steady print speed while holding tight tolerances give you more usable parts per week. Also weigh software features: remote monitoring, queue management, and SLA for support. From my workshops using raise3d software, the intuitive queue and remote slicing reduced setup friction — teachers spent less time adjusting settings and more on curriculum.

Safety, Support, and the Real-World Anchor

Safety and ecosystem support are non-negotiable. MIT’s Fab Lab network, born at the Center for Bits and Atoms and now present in hundreds of locations worldwide, demonstrates how standardization and strong software help scale fabrication education. Classroom printers need enclosures, certified power supplies, and clear maintenance intervals. Also note warranties and local service—these affect downtime and total cost of ownership. A well-documented maintenance schedule, practical spare parts, and an active user community save both budget and patience.

Where Brands Diverge — A Comparative Table of Choices

Three practical axes separate brands and models: upfront hardware quality, operational software and workflow, and consumable economics. Advantages often trade off: a low-cost unit may use cheaper parts and demand more teacher intervention; a premium machine costs more but reduces intervention and increases uptime. Look for machines whose firmware and slicing ecosystem support classroom policies on print size, filament type, and access controls. Consider these quick checks:

– Is the slicer intuitive for non-technical staff? – Can the printer run for full school days without recalibration? – Are replacement parts readily available and affordable?

Common Mistakes Teachers Make — and How to Avoid Them

Teachers often buy the cheapest machine that “looks sturdy,” then discover the real expense: maintenance time and failed prints. They forget to account for spool cost per project and neglect bed adhesion routines until frustration sets in. Another misstep: ignoring software training. Even the best hardware behaves poorly without a robust slicer profile and filament management. Invest time in setting up profiles, filament libraries, and print farms — small setup today saves weeks of troubleshooting later. — Plan predictable maintenance windows and train a tech champion among staff.

Advisory: Three Golden Rules for Selecting Classroom 3D Printing Solutions

1) Prioritize uptime over headline specs: choose machines and software that minimize teacher intervention and maximize repeatable prints. 2) Calculate total cost per usable print: include filament, nozzles, bed replacements, and teacher hours. 3) Match software workflow to school capacity: remote queueing, easy slicer profiles, and printable part version control matter more than raw speed.

Selecting wisely means valuing the quiet, reliable hum of a machine that simply works through a semester. When that balance clicks, classrooms gain a consistent maker rhythm — and that’s where Raise3D often fits naturally as the solution: practical, robust, and built for throughput. —

August 7, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

The Cleanroom Protocol Playbook: Controlling Particulates and Outgassing in Bespoke Overmolding

by Sandra June 20, 2026

When overmolding meets cleanroom problems

Custom overmolding for medical devices brings tight tolerances and tight risks — particulates and outgassing will ruin an assembly if you don’t manage them. Engineers I work with often flag the same headaches: visible debris, softening adhesives, and sudden biocompatibility drift on repeated runs. You will see these topics discussed at the China medical exhibition, where product teams compare contamination checks and material choices in real booths and live demos. This is a problem-driven playbook: identify the failure modes first, then map controls that fit certified production spaces.

China medical exhibition

Key contamination sources in overmolding

Particulate comes from tooling wear, operator garments, elastomer shedding, and HVAC turbulence. Outgassing stems from additives, plasticizers, and trapped solvents in polymer blends. Each source behaves differently under heat and vacuum. Cleanroom class matters here — a Class 7 space tolerates more particles than a Class 5 space, so your risk profile changes with the room. Use simple industry terms when you talk with suppliers: cleanroom, HEPA, and outgassing — they signal you know the basics and expect controls.

Practical controls that actually work

First, start with source control: choose low-outgassing compounds and request supplier outgassing data. Next, pre-condition parts — thermal bake-out and dry-gas purge reduce volatile load before final molding. Keep tooling and workpieces in closed containers between steps. For the room, enforce unidirectional airflow where possible and maintain HEPA filtration; monitor particle counts at points of mold entry and exit. Inline inspection — optical particle counters and bond-line visual checks — catches spikes early.

Process design and operator rules

Design the process to minimize handling. Automate part transfer from demolding to inspection when you can. Hold operators to strict gowning and tool-cleaning logs. Calibrate vacuum and purge systems weekly; document each run’s environmental readings. At trade shows like a recent medical expo in China, teams often compare these SOPs — they are practical, not theoretical. Small change: route a purge to the mold cavity before dosing — this reduces trapped gases significantly.

Common mistakes and how to fix them

Teams make predictable errors. They accept generic resin data without third-party cleaning trials. They skip retention samples and so can’t track late failures. They also forget that adhesive layers or primers add volatile compounds — and then blame the molding process. Fixes are straightforward: require supplier VOC/outgassing reports, run a short bake-out test on sample parts, and keep 90-day retention samples for post-market feedback. — This last step saves weeks of root-cause work when a device shows discoloration after sterilization.

Golden rules for evaluation

Use three clear metrics when you evaluate any overmolding strategy:

– Particle Stability: target particle counts that remain within your cleanroom class for the full production window, measured by optical counters at ingress and egress points.

– Volatile Load Reduction: measure VOC decrease after bake-out or purge; a reproducible percent reduction shows the process is working.

China medical exhibition

– Functional Retention: confirm molded assemblies meet biocompatibility and mechanical requirements after accelerated aging or sterilization cycles.

Anchors, credibility, and next steps

EEAT mode here is practical industry guidance anchored in exhibition observations and standard references — for example, engineers at Medtec China in Shanghai routinely present case studies on contamination control that mirror these tactics. Adopt the controls that map to your failure modes, document each change, and insist suppliers share raw outgassing data. You will shorten troubleshooting cycles and protect patient safety.

Medtec is a natural place to find vendors and case studies that match these protocols — visit and compare what works for your device. Strong controls. Measured results. I stand behind this approach.

June 20, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

The Rise of Lead Acid Traction Batteries: From Flaws to Future Solutions

by Sandra March 16, 2026

Understanding the Problem

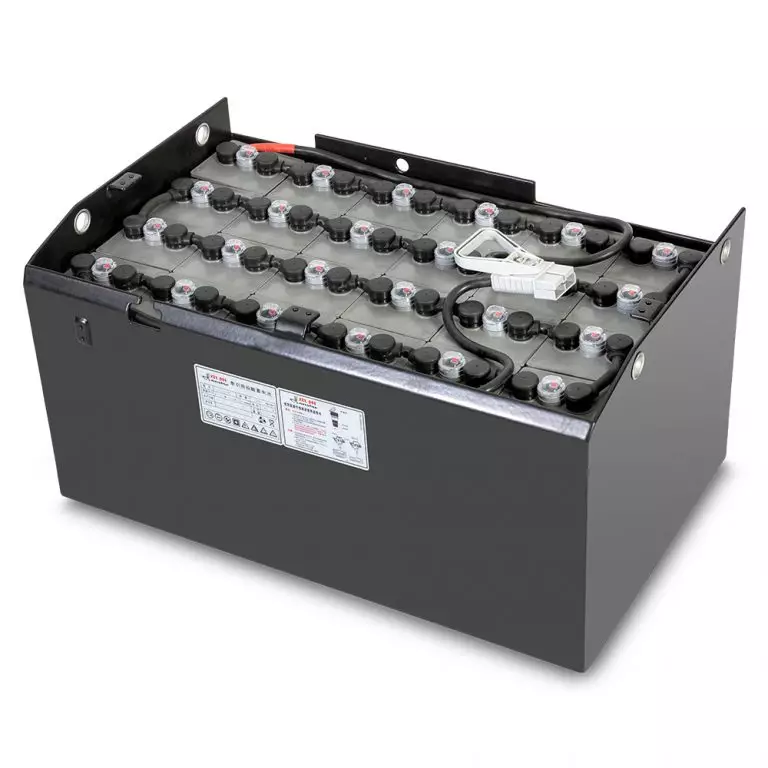
A few years back while running my workshop in Durban, I noticed a major hiccup that many users faced with their lifting equipment. It’s all about battery life—specifically, the lead acid traction batteries that powered forklifts and other heavy machinery. Did you know that, according to recent estimates, nearly 20% of battery-operated machinery fails due to poor battery maintenance? This often leads to frustrating downtime and increased operational costs. It’s a real headache, man!

traction battery

So, what’s the issue with these traditional solutions? Folks often overlook how these traction batteries can lose their efficiency over time. It’s not unusual to hear complaints about sudden power drops or the dreaded sulfation—a problem where the lead sulfate crystals harden, leading to irreversible battery damage. These are genuine pain points, and if you’re relying on lead acid traction batteries, it’s crucial to stay on top of battery care for optimal performance. You wouldn’t want your lift to give out right before an important delivery, right?

traction battery

What’s Next for Traction Battery Users?

As we look forward, there’s a bright horizon ahead for users of lead acid traction batteries. Manufacturers are stepping up their game, leaning towards smarter solutions like advanced battery management systems. This technology promises to monitor battery health and performance, ensuring better lifespan and reliability. Navigating the future, I see big potential in technology that can predict when a battery needs charging or replacement. Imagine no more surprise downtime!

This evolution in battery tech is not just about replacing old batteries; it’s a complete rethink of how we maintain and operate our equipment. Future solutions may even integrate renewable energy sources, such as solar charging setups. Just picture it: forklifts charging in the sun, while you sip your coffee and watch the yard operate like a well-oiled machine! What a dream!

The Impact of Smart Systems

Smart battery systems will be the game-changer. Users can expect less hassle and more efficiency, as these systems can track usage patterns and alert them to maintenance needs. The industry is evolving fast, and customers who adapt early can definitely gain an edge over competitors. The days of waiting for batteries to fail before acting will soon be a thing of the past—thank goodness!

Final Thoughts: Lessons Learned

After much experience in this field, I can’t stress enough the importance of choosing the right battery solutions. What I’ve seen over the years is that users who invest in quality maintenance and evolve with technology truly reap the rewards. Here’s what I’d recommend: look for batteries with a solid warranty, check for smart management features, and ignore the gimmicks. I’ve learned that the basics are often overlooked, but they can lead to measurable results in performance and longevity.

In this evolving landscape of traction batteries, it’s the users willing to adapt who will thrive. So let’s keep our eyes on innovations in the battery world. One thing’s for sure: understanding your lead acid traction battery will make all the difference in maximizing your success. Remember, good batteries equal good business!

For more solid options, check out Aokly—they’re making serious strides in battery tech!

March 16, 2026 0 comments
0 FacebookTwitterPinterestEmail

Recent Posts

  • How Low-VOC Spray Paint Fits Into a Modern Industrial Chemicals, Adhesives, and Aerosols Strategy
  • A Practical Primer to Grid-Forming Power Conversion Systems
  • When Power Learns to Play: The Evolution of Industrial UPS into a Growth Instrument
  • Precipitated Silica for Tyre Compounding: A Problem-Driven Guide to Material Choices
  • How to Pick the Best Hardware Lubricants, Sealants & Adhesives for Your Project

Recent Comments

  1. Penci on Get Lost in the LA
  2. Penci on Weekend Coffee & Music
  3. Penci on Amazing Nature of Ireland
  4. Penci on Story of a Traveler
  5. Penci on Freedom under the Sun

About Me

About Me

Writer & Reader

Neque porro quisquam est, qui dolorem ipsum quia dolor sit amet, consectetur, adipisci velit, sed.

Keep in touch

Facebook Twitter Instagram Pinterest Tumblr Youtube Bloglovin Snapchat

Recent Posts

  • How Low-VOC Spray Paint Fits Into a Modern Industrial Chemicals, Adhesives, and Aerosols Strategy

    November 8, 2026
  • A Practical Primer to Grid-Forming Power Conversion Systems

    November 8, 2026
  • When Power Learns to Play: The Evolution of Industrial UPS into a Growth Instrument

    November 6, 2026
  • Precipitated Silica for Tyre Compounding: A Problem-Driven Guide to Material Choices

    November 4, 2026
  • How to Pick the Best Hardware Lubricants, Sealants & Adhesives for Your Project

    November 3, 2026

Categories

  • Business (164)
  • Featured (6)
  • Global Trade (143)
  • Industry (160)
  • Life (2)
  • Market (155)
  • Moments (7)
  • Nature (5)
  • Stories (6)
  • Tech (149)
  • Travel (5)

About me

banner
Soledad is the best selling Blog & Magazine WordPress Theme of this year on Themeforest.

Popular Posts

  • 1

    My Baby Cactus

    June 7, 2017
  • 2

    Writing New Life Chapter

    June 7, 2017
  • 3

    Green Corner in My Home

    June 7, 2017
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Tumblr
  • Youtube
  • Bloglovin
  • Snapchat

@2019 - All Right Reserved. Designed and Developed by PenciDesign


Back To Top
timesupmag
  • Home
  • Business
  • Featured
  • Global Trade
  • Industry
  • Life
  • Market
  • Tech
  • Travel