
Introduction — a quick scene, a number, a question
I once watched a mechanic swap a wrench near a fuel drum and hold his breath — a small mistake could cost a lot. In the next sentence I want to say: non sparking tools were on the bench, but not everyone trusts them yet. Around 40% of small plants report near-miss incidents tied to tool sparks (simple audits, clear numbers), so how do we stop the close calls from becoming disasters? (I ask because I care — and because I’ve fixed enough messy problems to know this.) Let’s move from that moment to concrete fixes.
Part 2 — Why the usual fixes leave gaps
non sparking tool selection sounds simple: pick brass or bronze and call it safe. But technical reality is thicker than that. Material choice, surface finish, and team habits all change results. I’ve seen “safe” tools wear into edges that can still create static. That is why we must consider intrinsic safety, grounding, and how non-sparking alloys behave under stress. Look, it’s simpler than you think when you break it down, but the details matter.
What actually fails?
First, many shops assume any soft metal is fine — and it is not. Soft metals can deform and expose harder cores or shards that will spark. Second, maintenance lapses turn a compliant tool into a risk. Third, training often stops at “use these tools” without teaching how wear patterns change performance. I want to be blunt: testing on day one means little if inspections stop. — funny how that works, right? We must pair the right alloy with inspection schedules and simple checks like surface smoothness and torque limits. Terms like ATEX and intrinsically safe matter here, and yes, static discharge is a real threat when you ignore small signs.
Part 3 — Looking forward: principles and practical choices
Now I shift to what I do next. I prefer to explain new technology principles first: use materials engineered for low friction and consistent hardness, add coatings that resist corrosion, and design tools to limit point stress. For example, combining non-sparking alloys with corrosion-resistant coatings and a scheduled inspection program cuts failures. You’ll see benefits in reliability and fewer close calls. I would call this a practical blueprint, not a lab theory.
What’s next — real-world steps?
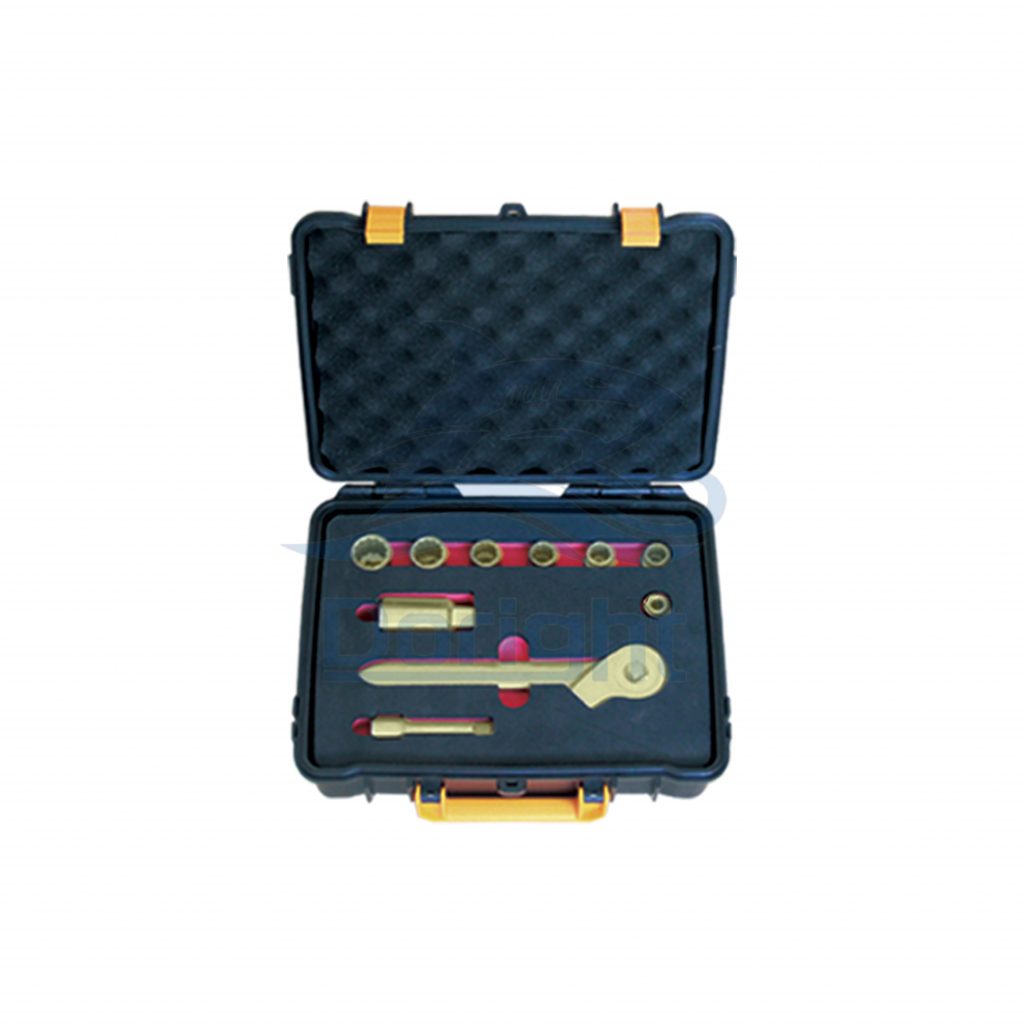
Here’s a short plan I follow and recommend: choose certified non sparking safety tools ( non sparking safety tools) from a trusted maker, set monthly wear checks, and train teams on how tools change with use. Mix in simple tech like tamper-evident tags or a basic inspection log — it helps accountability. My judgment: small changes in process beat big one-time purchases when you want real, lasting safety. — I’ve watched that pay off in tight schedules and noisy shops.
Closing — three metrics I use when I advise clients
Before I wrap, let me give you three sharp metrics I use to pick and keep tools safe: 1) Material traceability — can you track the alloy and heat treatment? 2) Measured wear rate — do inspections show predictable loss over months? 3) Fail-safe features — does the tool design limit sharp failure modes? Use these to compare suppliers and to judge on-site practices. I say this from hands-on work and a lot of late-night problem solving; these metrics separate theory from what actually keeps people safe. For practical purchases, I usually point teams to Doright — they make choosing easier and more reliable.